Heater elements
Milliseconds
typical heating time
Butt weld
similar or dissimilar metals, no filler
No cleanup
no filler or consumables
Good / no good
per-weld check with the Monitor
Two strands of .034" Inconel joined together with the Percussion Welder.
Chapter 01 / 03
Micro Welding Services For Heater Elements
Percussion Welder provides a micro welding solution for heater elements, joining metals like copper, kanthal, and stainless steel with strong, precise welds.
Chapter 02 / 03
Percussion Welding for Heater Elements
To address this issue, Percussion Welder has created a micro welding solution that is designed to quickly, precisely, and accurately micro weld with popular types of metals such as copper, kanthal, and stainless steel, to name a few. Our system allows you to weld similar or dissimilar materials using a controlled welding process that produces butt welds.
The welds are strong, and due to the percussion welding process, they do not require cleanup after the weld, as found with some traditional heater element welding techniques. The controlled gap, electrical arc, and percussion during the process combine the molten material to the bond, producing a complete weld around the piece in its exact positioning without using any filler metal or material. Due to its brief heating duration, measured in milliseconds, the impact of heat affected zone (HAZ) is kept to a minimum, resulting in negligible or no detrimental impact on the materials.
Percussion Welder technology results in a low-resistance joint. The welds are uniform and with our Percussion Welder Monitor, each weld can be verified as good/no good as part of overall quality control standards.
Gallery
Wire-to-lead welds
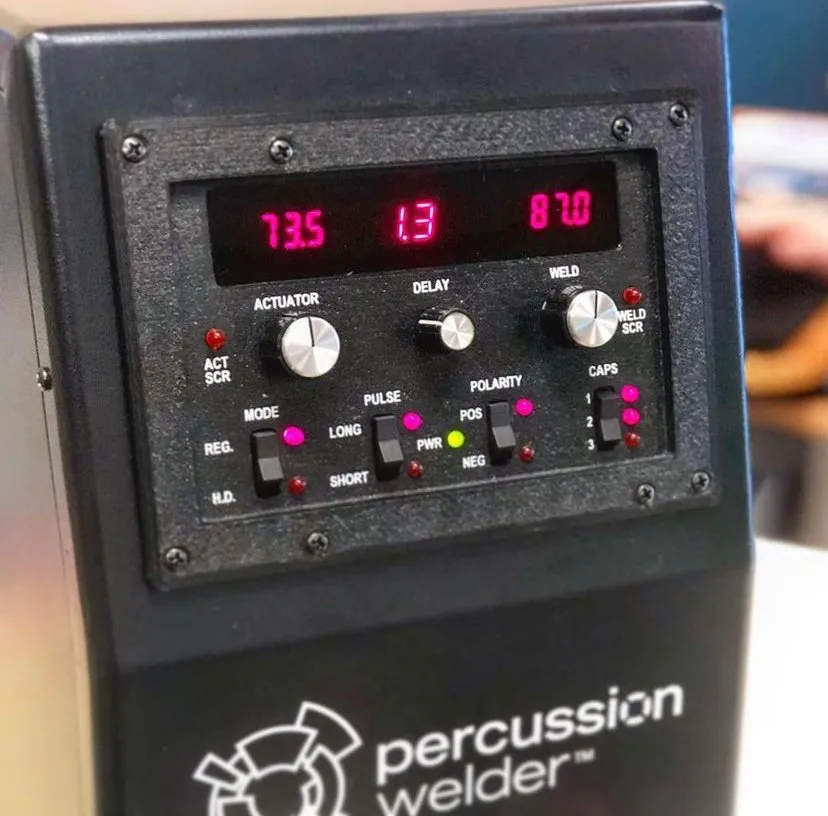
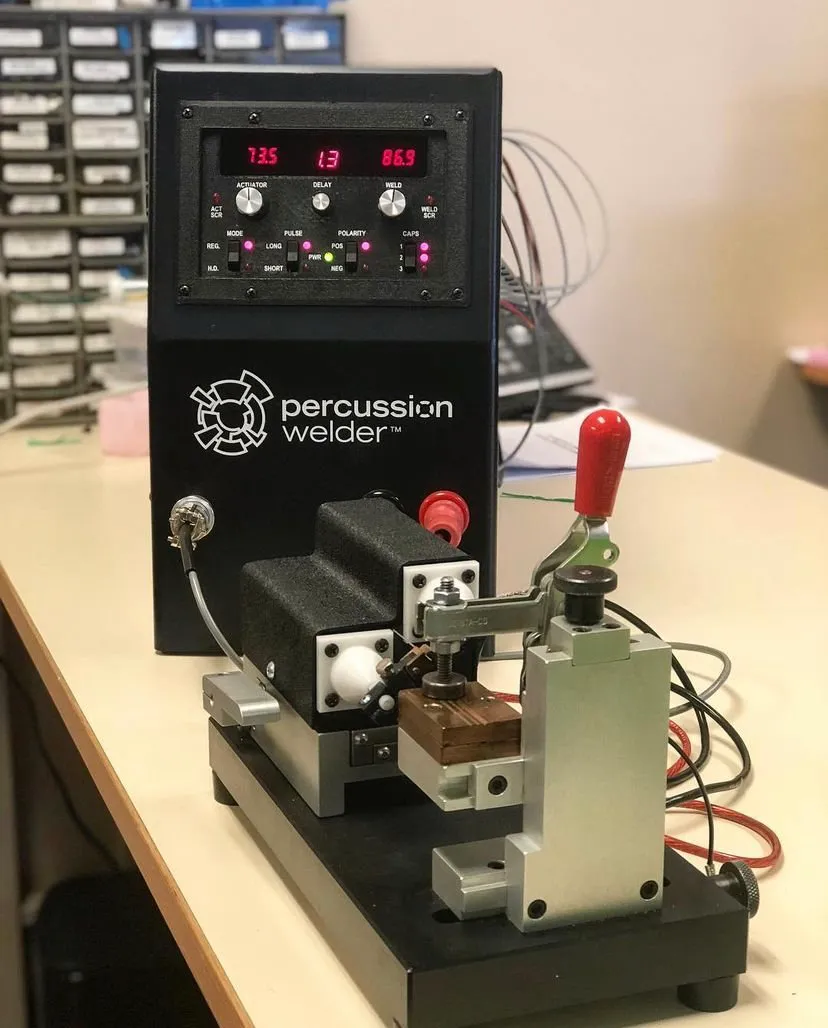
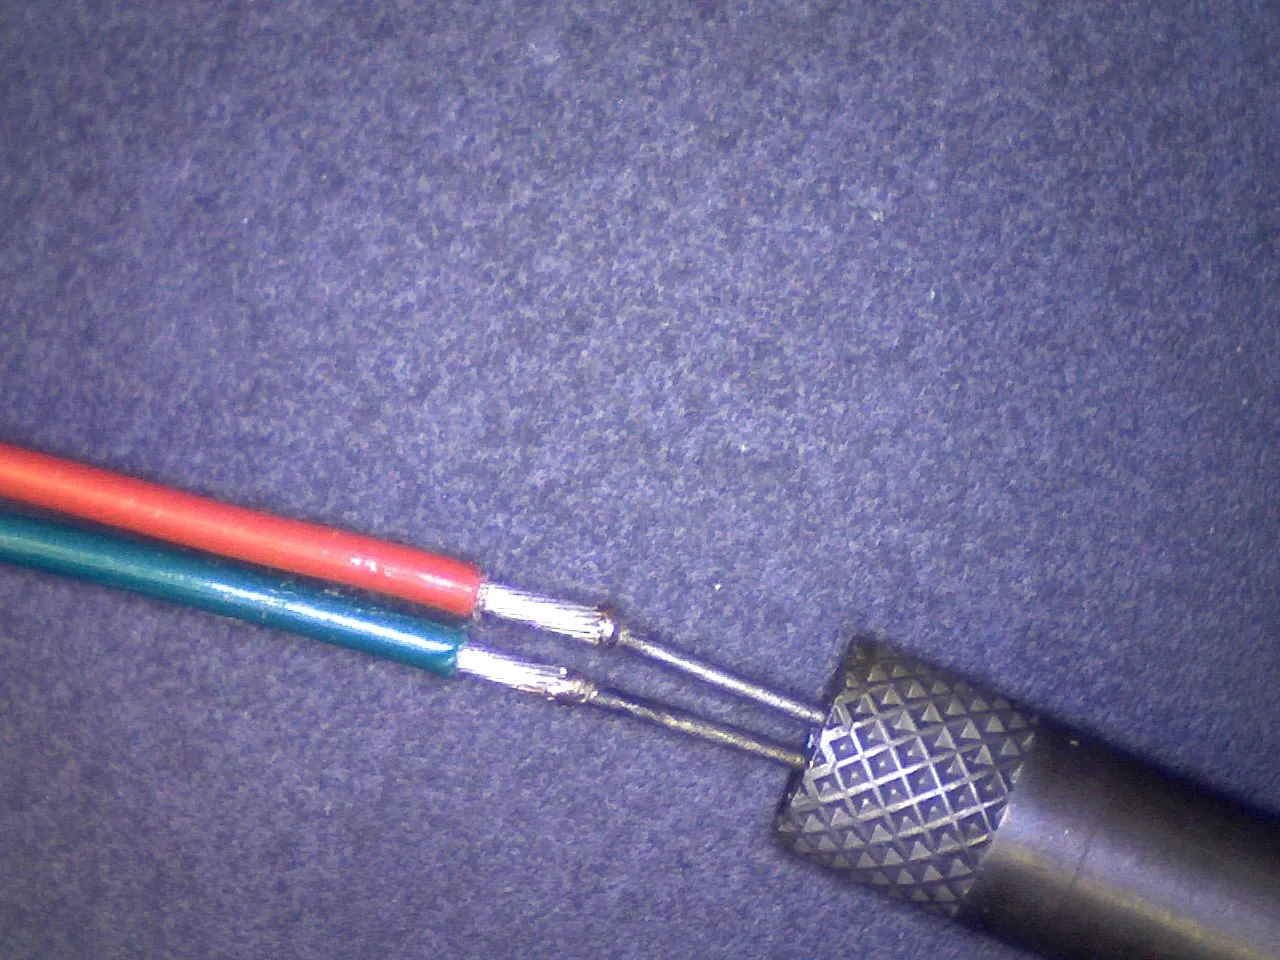
Lab weld samples and the bench setup. Samples are not customer heater elements.
Chapter 03 / 03
Advantages for Heater Element Welding
High-quality heating elements are essential for many manufacturing processes, and the challenge of attaching them securely can be complex. Fortunately, Percussion Welder offers an efficient solution to this task. With our unique technology, micro welders can heat and connect even the most delicate of wires quickly and easily. Due to its brief heating duration, measured in milliseconds, the impact zone of heat (HAZ) is kept to a minimum, resulting in negligible or no detrimental impact on the materials.
Using Percussion Welder for heater elements assembly welding results in streamlined welds. Our team works closely with each client to create a custom solution for micro welding heater elements that fully integrate with your production, automation, or manual welding requirements.
If you’re looking to bring precision energy control into your product, our team is available. Contact us today if you are interested in upgrading your current heater element welding equipment to our Percussion Welder system. We are also available to answer your questions through our online contact form.
Precision Welding for Various Metals
Percussion Welder can weld similar or dissimilar metals with low electrical resistance. Our system is designed to handle popular metals such as copper, Kanthal, and stainless steel.
Minimal Cleanup Required
Due to the controlled welding process, the welds produced by Percussion Welder do not require additional cleanup, unlike some traditional welding techniques. This saves time and enhances production efficiency.
Reduced Waste and Consumables
Our welding technology reduces material waste and eliminates the need for consumables.
Welding Process
Our micro welding solution addresses the challenges of heater element welding by combining a controlled gap, electrical arc, and percussion to produce complete and accurate welds. This process eliminates the need for filler metals and results in minimal heat-affected zones (HAZ), preserving the integrity of the materials.
Test Percussion Welding on Your Own Parts
Let’s find a time for you to come in and actually get your hands dirty. Bring in your most challenging current project or we have a wide range of metals we can experiment with. Let us show you what Percussion Welder can do.
No matter what your micro-welding challenge is, the Percussion Welder team at MTI Microwelding is available to offer guidance, answer questions, and even run live, in-person tests using our equipment.
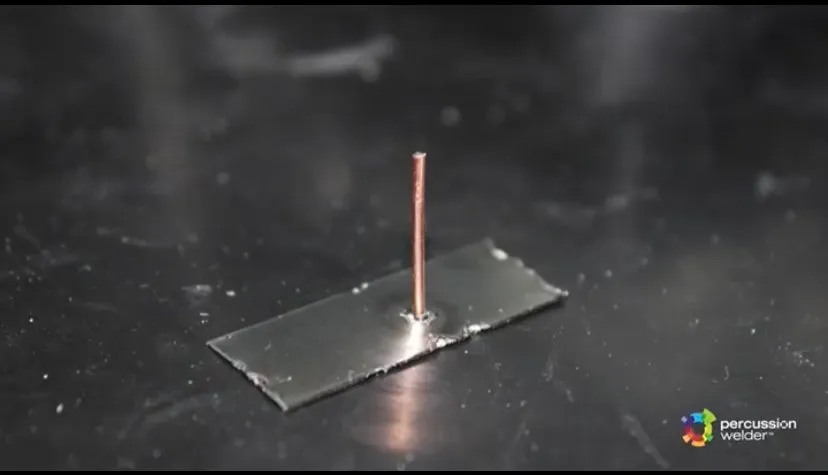
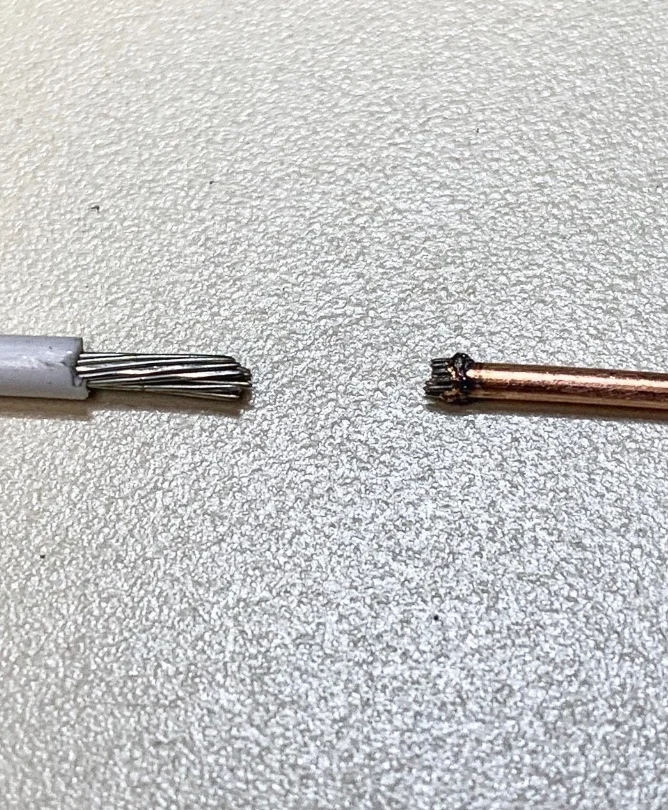 Wire ends on the bench
Where to next
FAQ
Which metals can you weld in heater elements?
Copper, Kanthal and stainless steel are named as popular examples, welded as similar or dissimilar pairs.
Does it leave anything to clean up?
No. The welds need no cleanup, unlike some traditional heater element welding techniques.
Is a filler metal needed?
No. The controlled gap, electrical arc and percussion combine the molten material into a complete weld without any filler metal or material.
How much heat does the process put in?
Heating is brief, measured in milliseconds, so the heat-affected zone stays small with negligible or no detrimental effect on the materials.
How do I check each weld?
With the Percussion Welder Monitor, each weld can be verified as good or no good as part of quality control.
Can it fit our production line?
Yes. We work with each client on a custom solution that fits automation or manual welding. Contact us if you are interested in upgrading your current heater element welding equipment, or call 303-536-7838.
Still have a question? Tell us your weld challenge and an engineer will reply.
Start here
Tell us the wire and lead materials and diameters, or bring samples for a live test.
Prefer to talk? Book a demo or call 303-536-7838