Equipment
X, Y, Z
alignment adjustments, plus a gap adjustment knob
Foot or hand
operator-selectable trigger
0-33 in/s
actuator speed across its voltage range
858 + 528/628
works with the 858; retrofits 528 and 628 systems with a kit
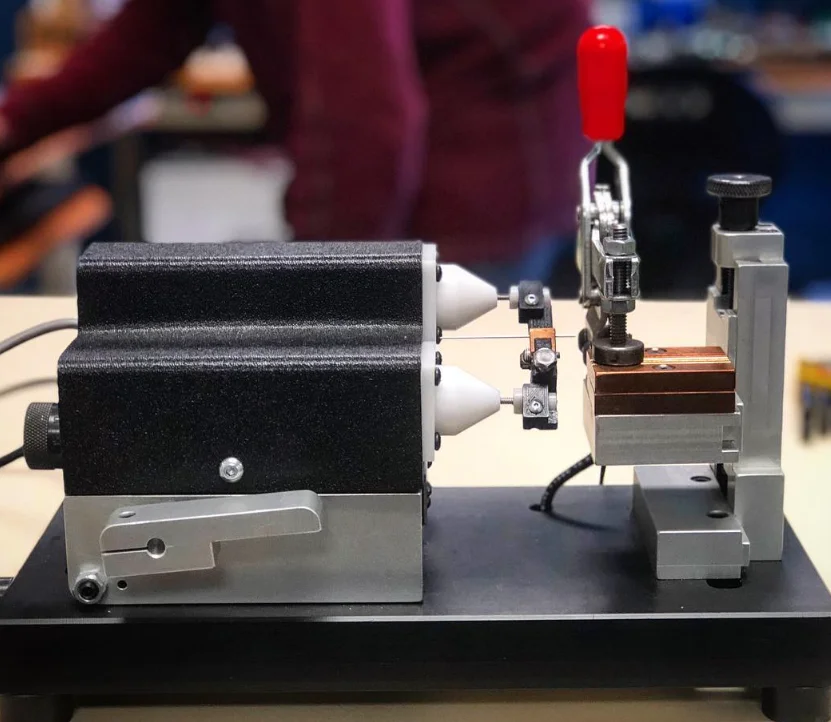 The 726 bench fixture
Anatomy
The 726 bench fixture, part by part
Tap a point on the fixture. It holds the weld materials, provides the alignment mechanism and applies the rapid motion.
Wire holder
Moveable wire holder
Holds the wire and thrusts it toward the workpiece. The thrust is spring-loaded.
Descriptions follow the 726 product page and diagram. Fixture details can vary by configuration.
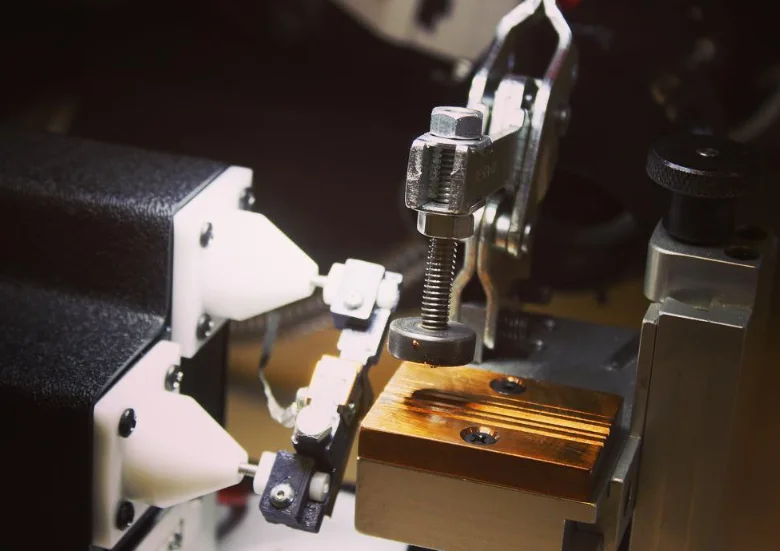 Cones, clamp and copper block
Chapter 01 / 08
What the 726 Bench Fixture does
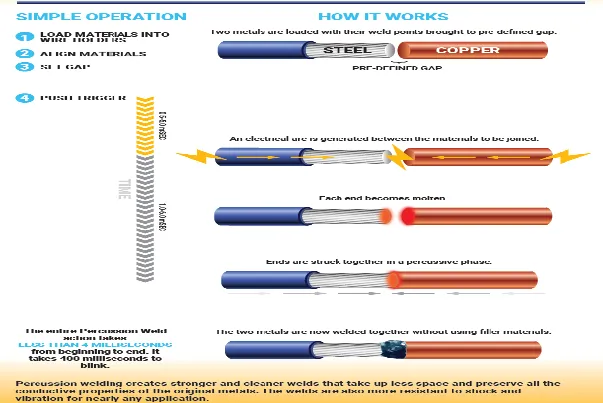
The 726 Bench Fixture is the “weld head” of the Percussion Welder system. It holds the two parts, aligns them to each other and thrusts one into the other when the weld is triggered. Together with the Model 858 Percussion Welder and the 808 Actuator, it provides what is needed to make consistent, reliable weld joints.
Percussion welding starts with the two parts set a pre-defined gap apart. When the weld is triggered, a capacitor-discharge arc melts the facing surfaces and the moveable part is driven into the stationary part, so the joint is made in milliseconds with no filler, flux or solder. The fixture is what makes the gap, the alignment and the motion repeatable from one weld to the next.
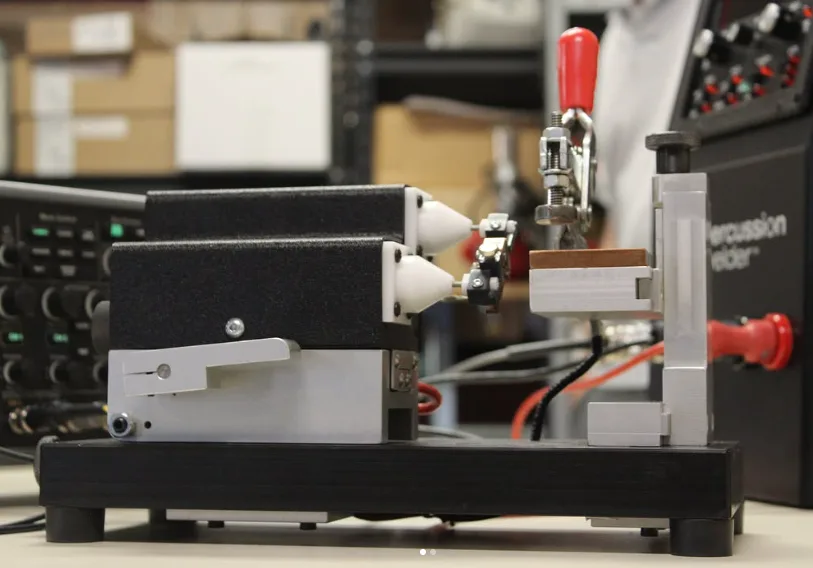 726 bench fixture, side view
Chapter 02 / 08
Anatomy of the fixture
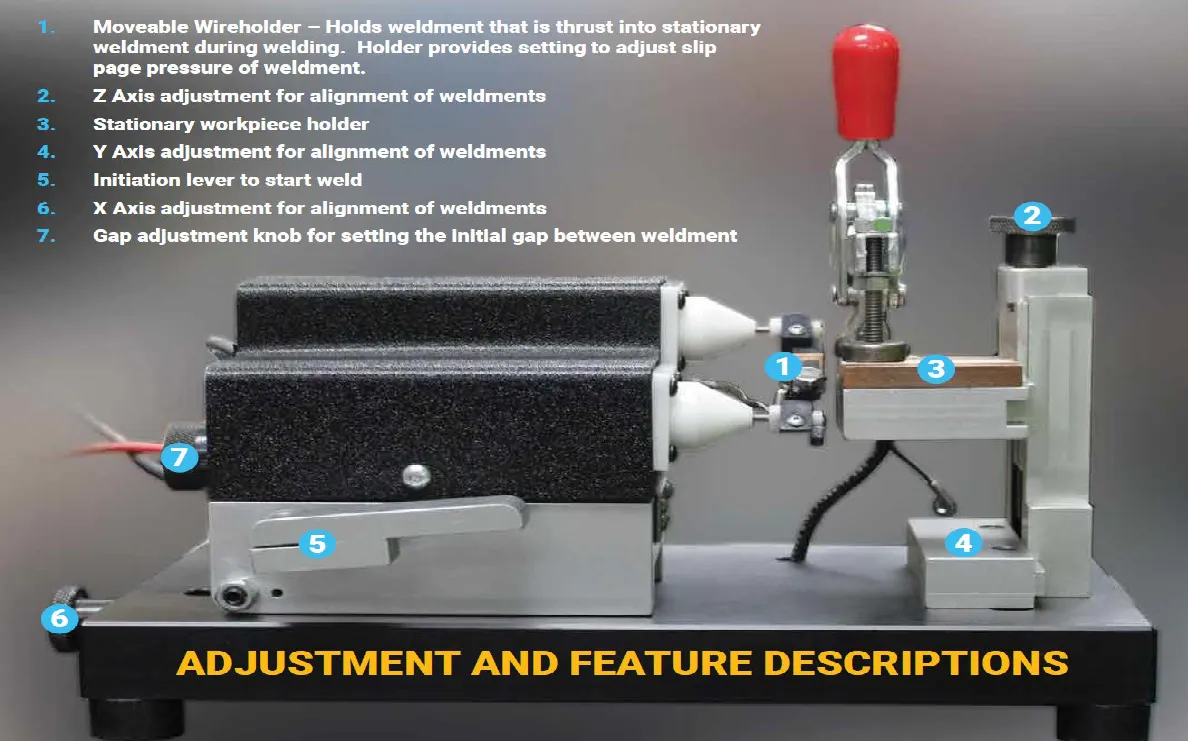
The diagram on this page numbers seven adjustments and features. In the order of the callouts:
- Moveable wireholder: holds the weldment that is thrust into the stationary weldment during welding, with a setting for the slippage pressure of the weldment.
- Z-axis adjustment: aligns the weldments vertically.
- Stationary workpiece holder: secures the workpiece during the weld.
- Y-axis adjustment: aligns the weldments horizontally.
- Initiation lever: starts the weld.
- X-axis adjustment: a third alignment adjustment for the weldments.
- Gap adjustment knob: sets the initial gap between the weldments.
Want to see it on your parts?
Send samples and we'll run test welds before you commit.
Gallery
Clamp, align, weld
The 726 from several angles.
Chapter 03 / 08
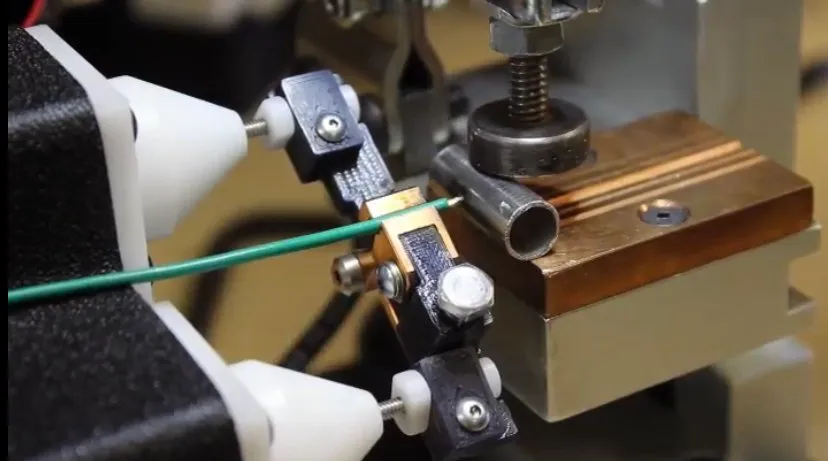
The moveable wireholder
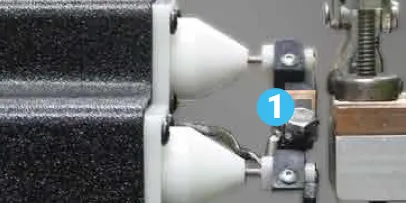
The moveable wireholder carries one of the two weldments and is the side that moves. During the weld it is thrust into the weldment in the stationary holder. The 808 Actuator supplies the rapid motion, and the holder uses a spring-loaded thrust mechanism.
The holder also has a setting for the slippage pressure of the weldment, so you can adjust how the part is held in it. As with every other setting, change one thing at a time and check the result on your own parts. Our lab weld schedules are starting points, not guarantees.
Chapter 04 / 08
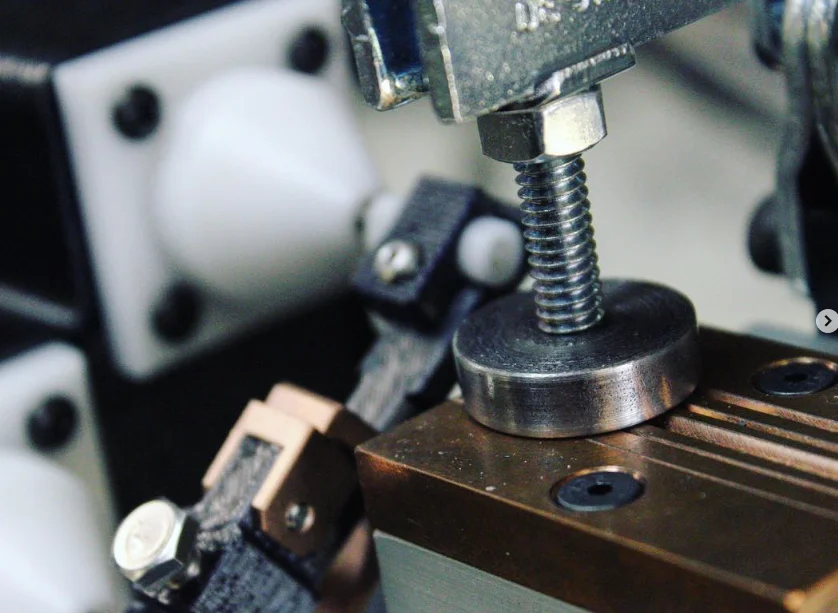
The stationary workpiece holder
The stationary workpiece holder secures the other weldment and keeps it still while the moveable part is thrust into it. In the photos it is the block with the red toggle clamp above it, with a clamp screw and pad that press the part against the block below.
It has an adjustable clamping system for wires, terminals, leads and small assemblies. Because the two sides of the joint are held separately, you can change the stationary part without disturbing the moving side. If your part has an unusual shape, ask us about custom tooling for your weld geometry.
 Clamp and copper block in the fixture
Chapter 05 / 08
Aligning the parts: X, Y, Z and gap
Alignment is set with adjustments on the fixture, so it can be repeated and written down rather than judged by eye each time.
- Z axis moves the weldments vertically relative to each other.
- Y axis moves them horizontally.
- X axis is the third alignment adjustment shown on the fixture diagram.
- Gap adjustment knob sets the initial gap between the weldments, the starting distance the parts travel before they meet.
Set the alignment and gap, run a weld, inspect it, then change one setting at a time. We recommend validating joint strength on your own parts before production.
Want to see it on your parts?
Send samples and we'll run test welds before you commit.
Chapter 06 / 08
Triggering the weld
The weld is started by the operator. The system supports a foot pedal or a hand switch, selected by the operator, and the fixture diagram labels an initiation lever that starts the weld. The 858 receives the trigger as a closed-contact input.
Operation is manual by default, and the fixture can be integrated into automated production lines with optional tooling. The video on this page walks through operating it step by step. If you plan to automate, tell us early, because it affects how the parts are fed and clamped.
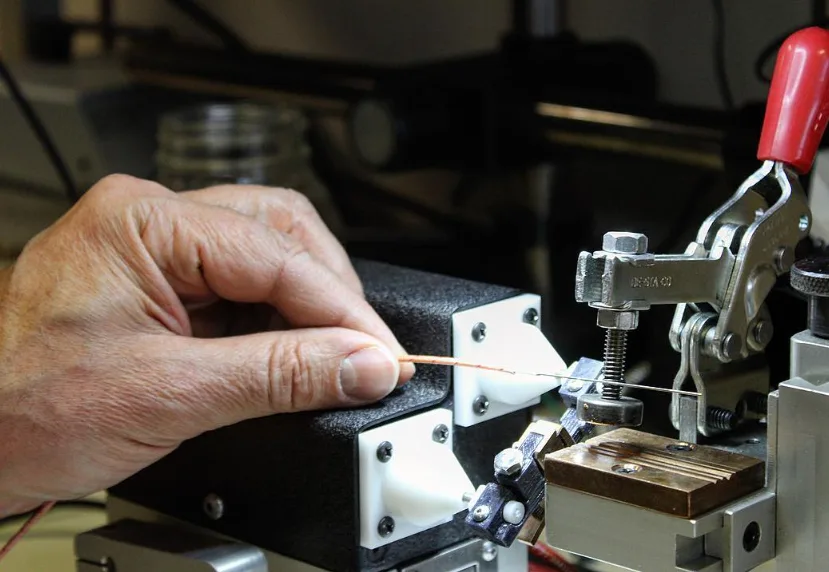 Loading a wire into the fixture
Chapter 07 / 08
Specifications
These are the 726 specifications we have confirmed. For anything not listed, such as overall dimensions or mounting, contact us.
| Compatible welder | Model 858 Percussion Welder; also retrofits 528 and 628 systems with an upgrade kit |
|---|---|
| Alignment | Z-axis and Y-axis adjustment; the diagram also labels an X-axis adjustment and a gap adjustment knob |
| Moveable wireholder | Spring-loaded thrust, with a slippage pressure setting |
| Stationary workpiece holder | Adjustable clamping system for wires, terminals, leads and small assemblies |
| Actuator speed | 0-33 in/s across the actuator's voltage range (808 Actuator) |
| Trigger | Foot pedal or hand switch, operator-selectable |
| Operation | Manual; can be integrated into automated production lines with optional tooling |
| Optional accessories | Percussion Weld Monitor for good/no-good checks; custom tooling for specific weld geometries |
| Built | Designed and manufactured in Denver, Colorado |
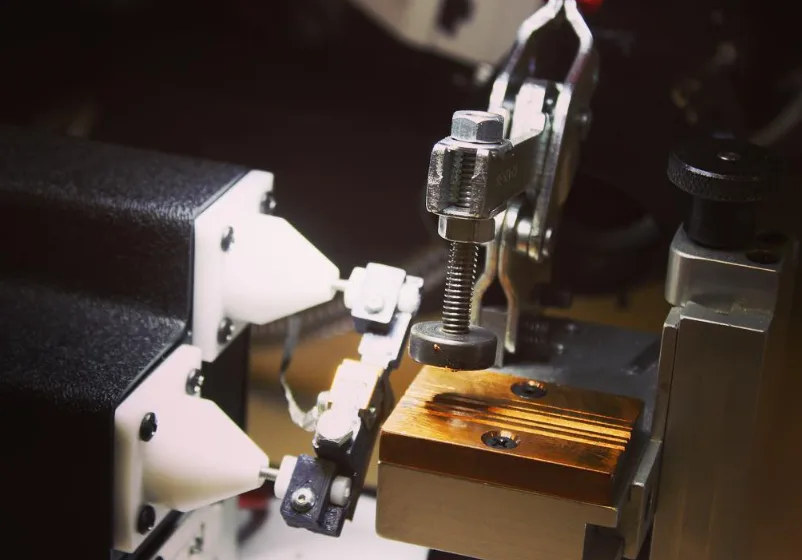 Inside the 726 fixture
Chapter 08 / 08
Part of the Percussion Welder system
The 726 is one of three parts of the system. The 858 is the controller and power supply, with dials for the actuator, delay and weld energy voltage and switches for mode, pulse, polarity and capacitance. The 808 Actuator provides the motion. The optional Percussion Weld Monitor compares each weld with a learned signature and gives a pass or fail.
If you run a Superior 528 or MTI 628, the 726 retrofits those systems with an upgrade kit. See the upgrade page.
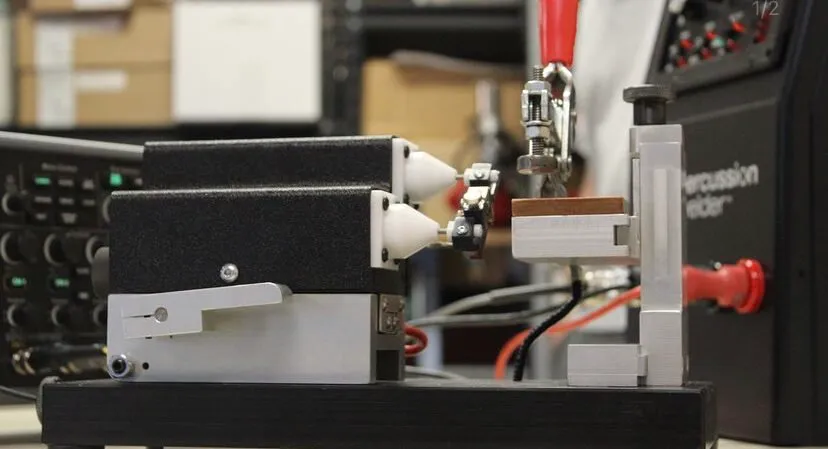
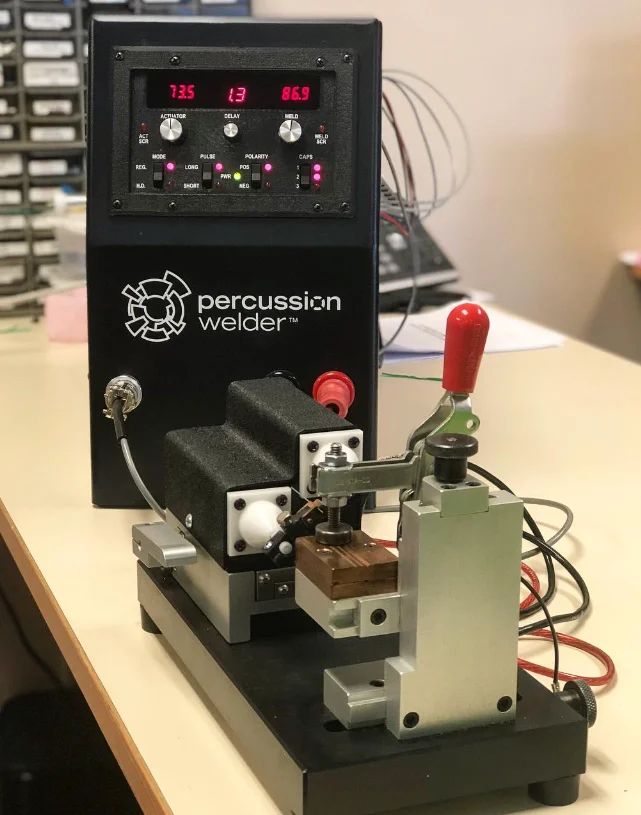 858 and 726 fixture on the bench
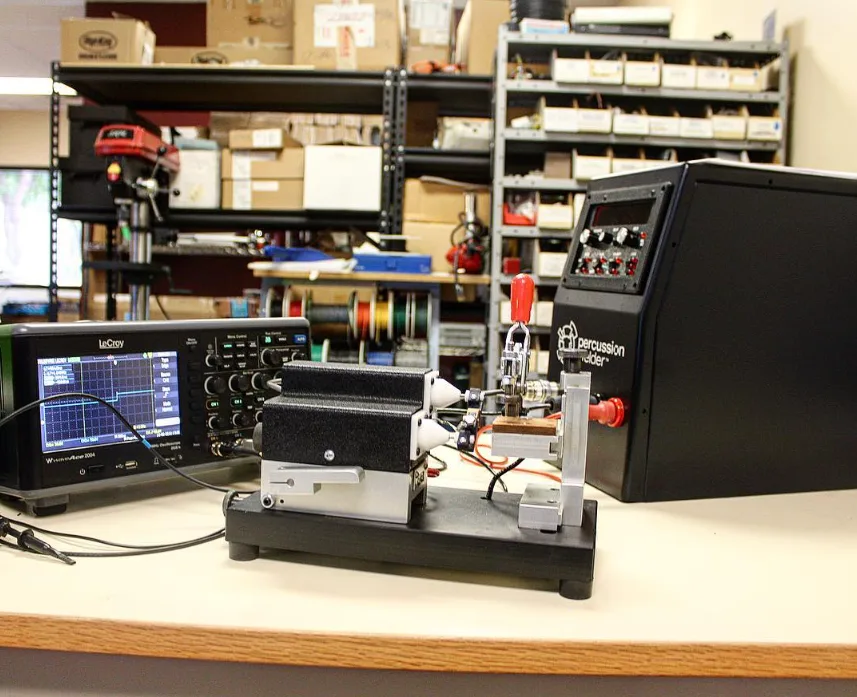 858, 726 fixture and oscilloscope on the bench
Where to next
858 Percussion Welder
The Model 858 is a capacitor discharge micro welder for thermocouple wire, fine wire and dissimilar metals. No filler, minimal HAZ. Call 303-536-7838.
Open →Actuator
The Model 808 Actuator is a low-mass solenoid built for percussion welding: 0.90 in stroke, speeds up to 33 in/s, driven by the 858 Percussion Welder.
Open →Percussion Weld Monitor
The Percussion Weld Monitor learns a signature waveform for your product, then tests production welds against it with pass/fail output and QC data.
Open →528 628 858 Upgrade
Running a Superior 528 or MTI 628? The Model 858 uses the same percussive-arc process with front-panel control. See what carries over, including weld schedules.
Open →FAQ
What does the 726 Bench Fixture do?
It is the weld head of the Percussion Welder system. It holds the two parts, aligns them to each other, sets the starting gap and thrusts the moveable part into the stationary part when the weld is triggered.
Which welder does it work with?
The Model 858 Percussion Welder. It also retrofits 528 and 628 systems with an upgrade kit. See the <a href="/528-628-858-upgrade/">528/628 upgrade page</a>.
How do I align the parts?
The fixture has Z-axis (vertical), Y-axis (horizontal) and X-axis adjustments for aligning the weldments, and a gap adjustment knob that sets the initial gap between them.
How is the weld triggered?
The system supports a foot pedal or a hand switch, selected by the operator. The fixture diagram also labels an initiation lever that starts the weld.
Can it be used in an automated line?
It is operated manually and can be integrated into automated production lines with optional tooling. Ask us about your line.
Can you test my parts in the fixture?
Yes. Free applications tests of your materials are available, and we can run live, in-person tests at our lab in Denver.
Still have a question? Tell us your weld challenge and an engineer will reply.
Start here
Bring a wire, lead or small assembly and we will set it up on the 726 in Denver. Free applications tests are available.
Prefer to talk? Book a demo or call 303-536-7838